 IN
Food Grade Packaging
370 products available
𝗪𝗵𝗮𝘁 𝗮𝗿𝗲 𝗙𝗼𝗼𝗱 𝗚𝗿𝗮𝗱𝗲 𝗣𝗮𝗰𝗸𝗮𝗴𝗶𝗻𝗴?
Food Grade Packaging refers to materials specifically designed to safely contain, protect, and preserve food products. These packaging solutions are made from approved substances that do not react chemically with food and are compliant with health and safety regulations. Food Grade Packaging plays a vital role in maintaining food quality, extending shelf life, and ensuring consumer safety.
The primary uses of Food Grade Packaging span various sectors within the food industry, including manufacturing, distribution, and retail. Businesses utilize these materials to package everything from raw ingredients to ready-to-eat meals. The demand for effective Food Grade Packaging has surged due to heightened consumer awareness regarding food safety and quality. As the global food industry continues to expand, the relevance of Food Grade Packaging in maintaining standards and compliance is more critical than ever.
𝗞𝗲𝘆 𝗙𝗲𝗮𝘁𝘂𝗿𝗲𝘀 𝗮𝗻𝗱 𝗦𝗽𝗲𝗰𝗶𝗳𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀
Food Grade Packaging offers numerous features and specifications tailored to meet industry needs. These specifications ensure that the packaging is not only safe but also functional and efficient for food storage and transportation.
Key specifications include:
1. Material Composition
- Typically made from polyethylene, polypropylene, or biodegradable options
- Must be free from harmful chemicals and contaminants
2. Barrier Properties
- Provides protection against moisture, oxygen, and light
- Helps in preserving freshness and quality for extended periods
3. Temperature Resistance
- Capable of withstanding varying temperature ranges for storage and transport
- Essential for frozen, refrigerated, and ambient products
4. Compliance Standards
- Must adhere to local and international food safety regulations
- Examples include FDA and EU regulations
5. Customization Options
- Available in various sizes, shapes, and designs
- Can be tailored to specific branding needs
6. Sustainability Features
- Many options are recyclable or made from renewable resources
- Aligns with eco-friendly practices and consumer preferences
7. Strength and Durability
- Designed to withstand handling and transport stress
- Reduces the risk of damages during distribution
8. Sealing and Closure Mechanisms
- Various options for secure sealing to prevent contamination
- Options include heat sealing, adhesive, or tamper-evident closures
These specifications ensure that Food Grade Packaging meets the diverse needs of the food industry, promoting safety and quality.
𝗖𝗼𝗺𝗺𝗼𝗻 𝗔𝗽𝗽𝗹𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀 𝗮𝗻𝗱 𝗨𝘀𝗲 𝗖𝗮𝘀𝗲𝘀
Food Grade Packaging is utilized across various industries to facilitate safe food handling and storage.
1. Food Manufacturing: Food Grade Packaging is essential in the production of processed foods, ensuring that ingredients remain uncontaminated during processing.
2. Food Distribution: Transportation of perishable goods relies on Food Grade Packaging to maintain product integrity and safety during transit.
3. Retail: Grocery stores utilize Food Grade Packaging for items like fresh produce, baked goods, and deli products to enhance shelf life and appeal.
4. Catering: Food service businesses depend on Food Grade Packaging for meal prep and delivery, ensuring hygiene and quality are upheld.
5. E-commerce: The rise of online food sales has increased the demand for effective packaging solutions that protect food during shipping.
6. Pharmaceuticals: Certain packaging solutions are also suitable for food-related pharmaceuticals, ensuring compliance with safety standards.
7. Snack Foods: Packaging for snacks often includes barrier properties to maintain freshness and prevent spoilage.
𝗣𝗿𝗼𝗱𝘂𝗰𝘁 𝗩𝗮𝗿𝗶𝗮𝗻𝘁𝘀 𝗮𝗻𝗱 𝗦𝘂𝗯𝗰𝗮𝘁𝗲𝗴𝗼𝗿𝗶𝗲𝘀
Food Grade Packaging encompasses a wide range of product variants to cater to different market needs.
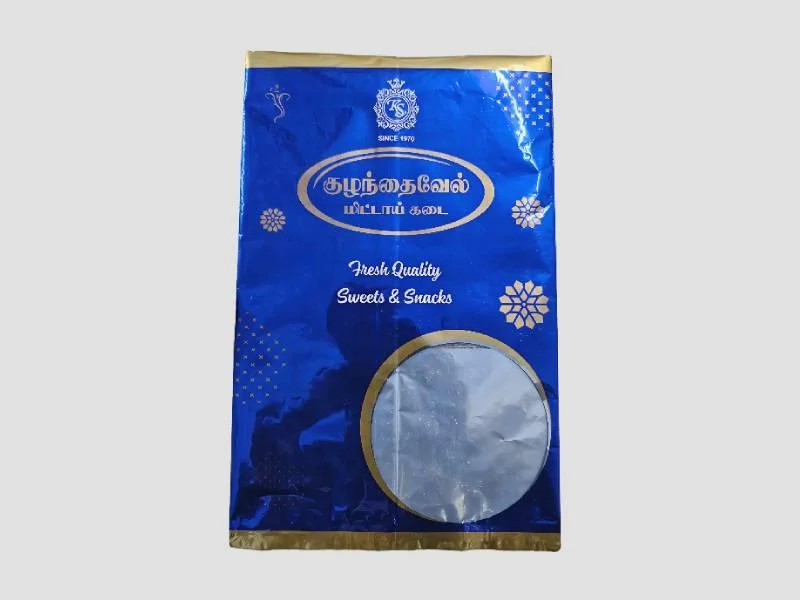
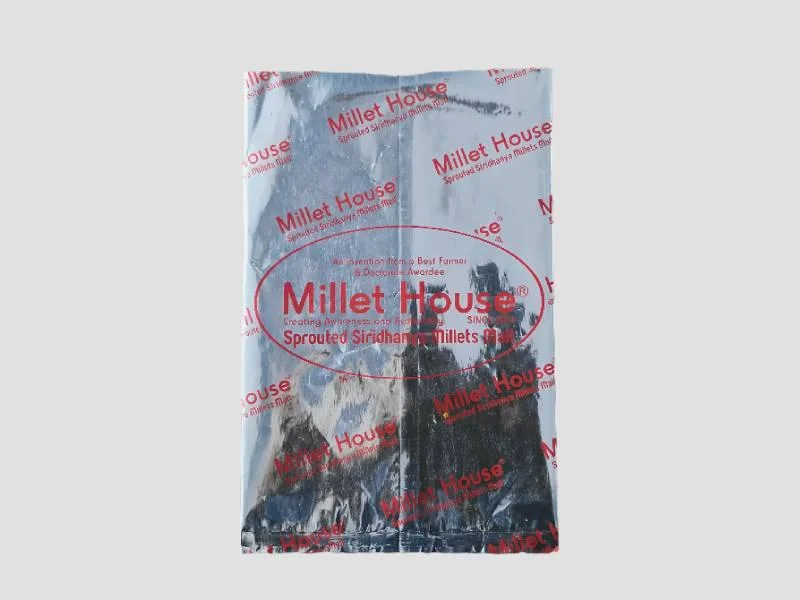
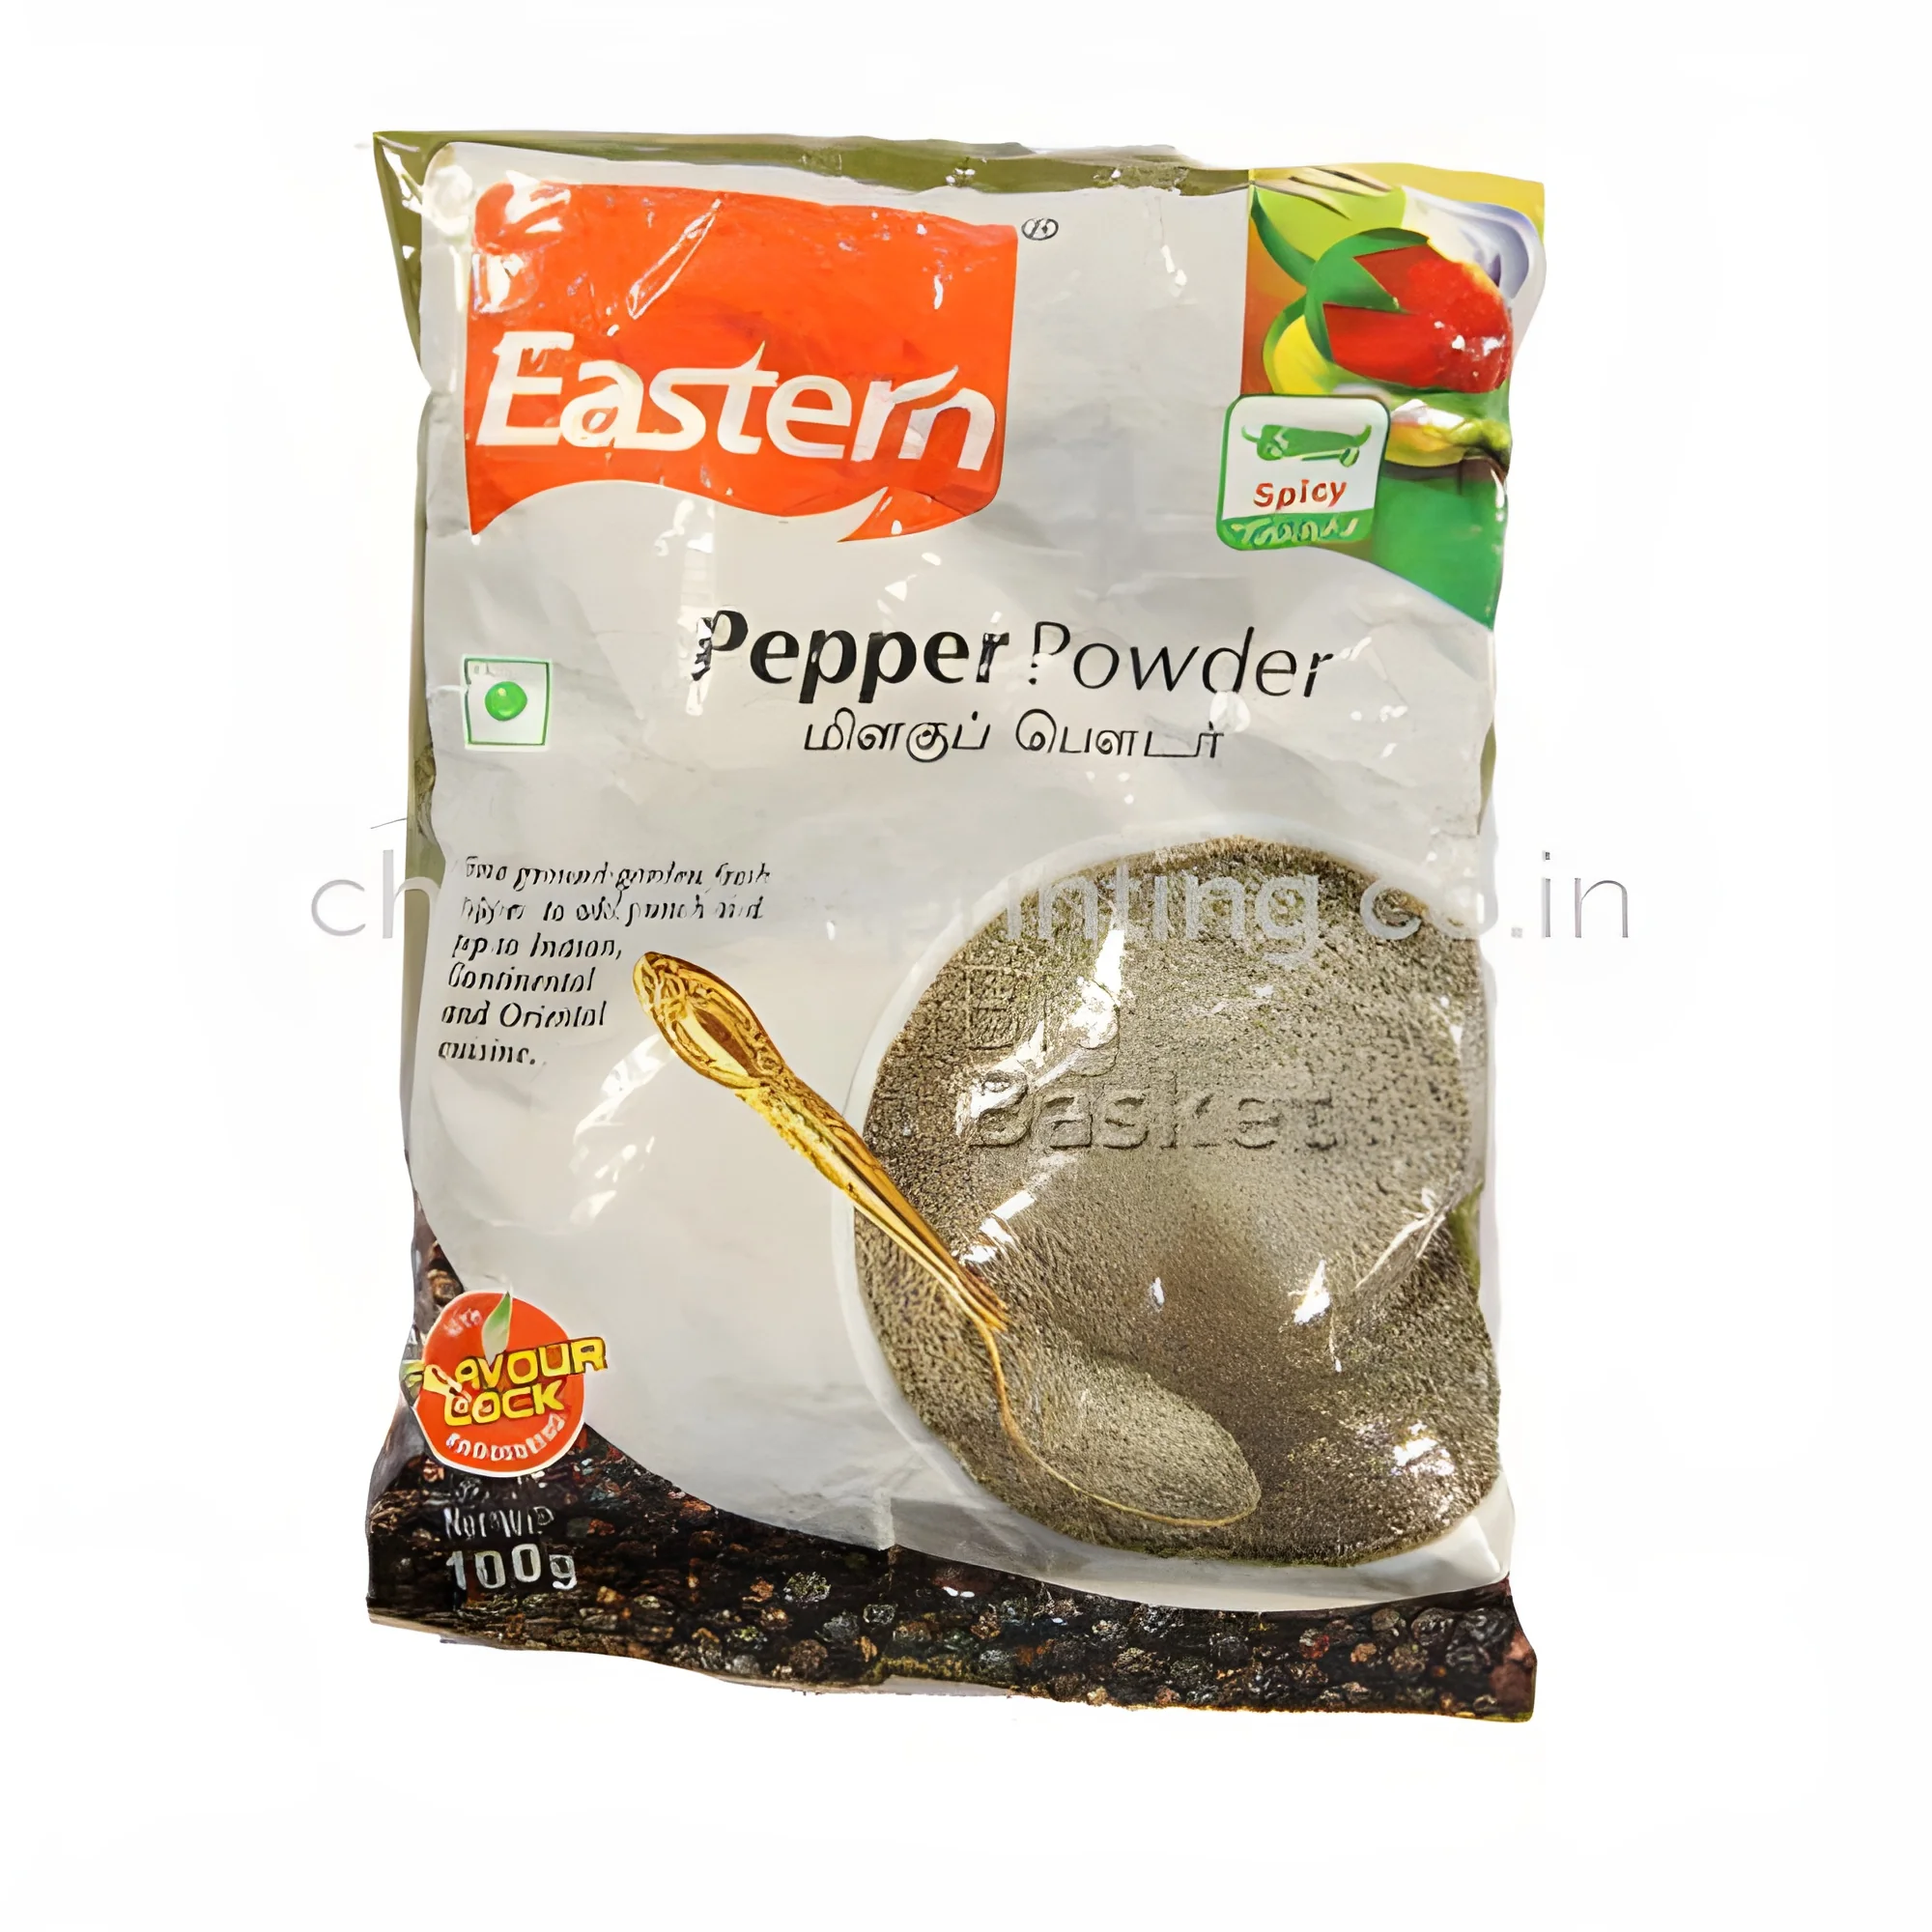
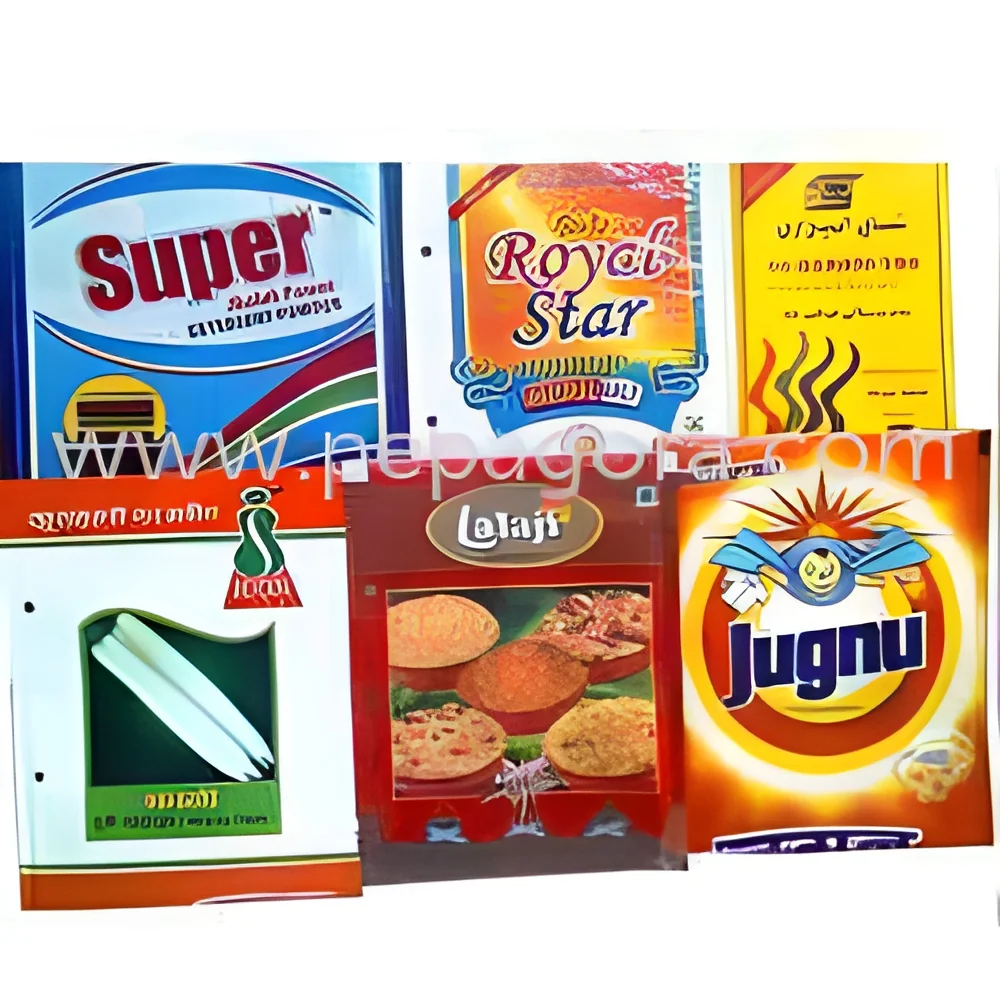
Pouches
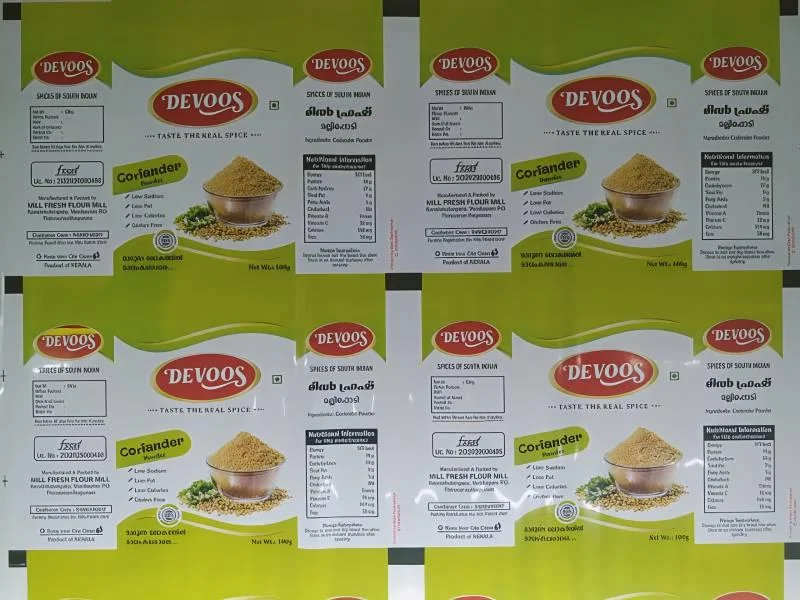
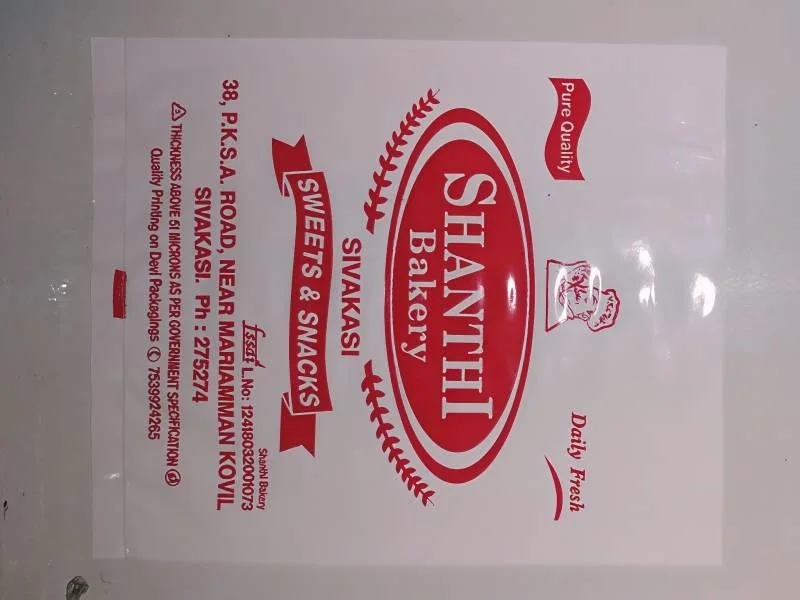
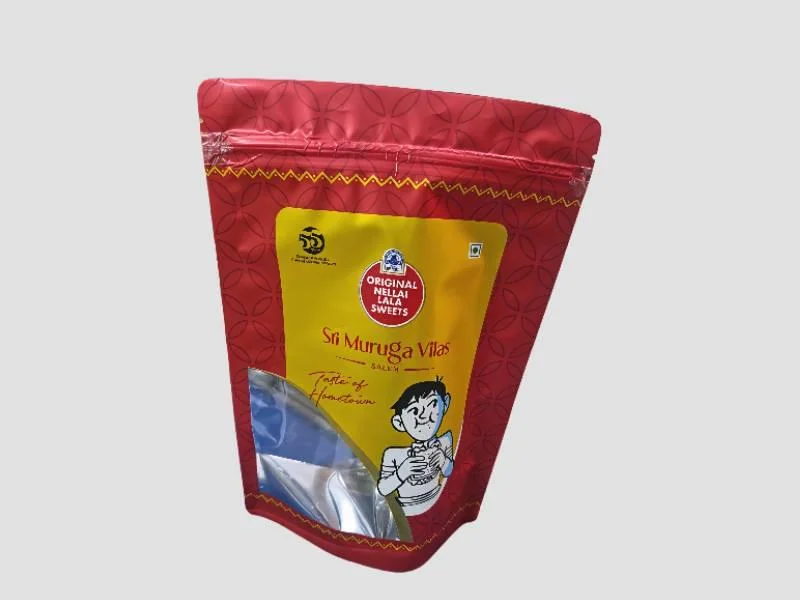
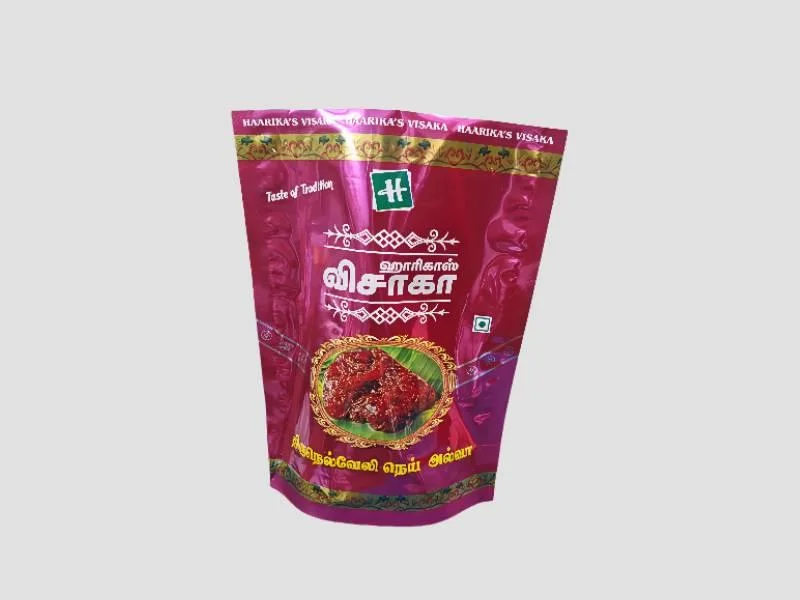
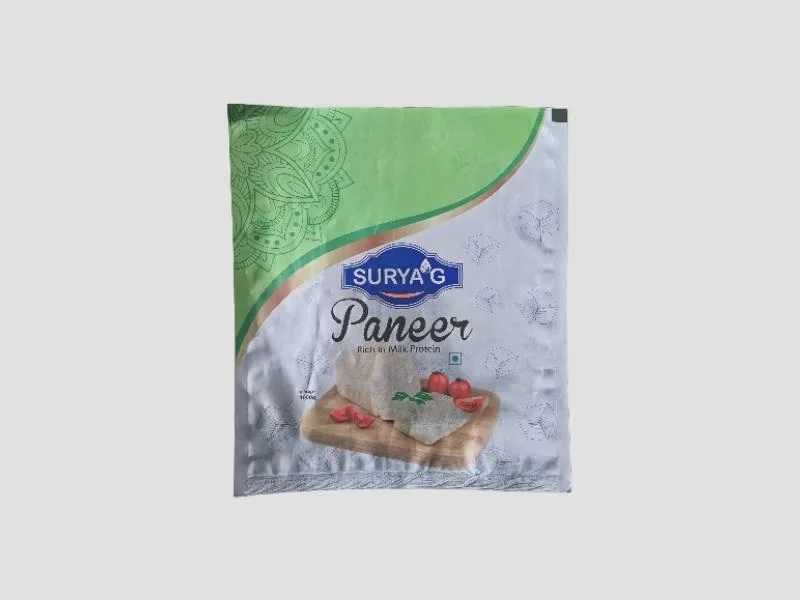
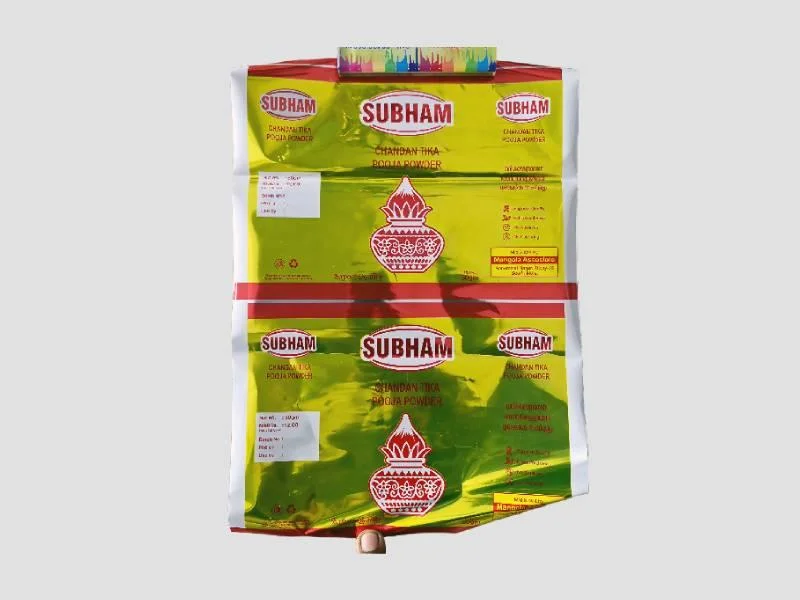
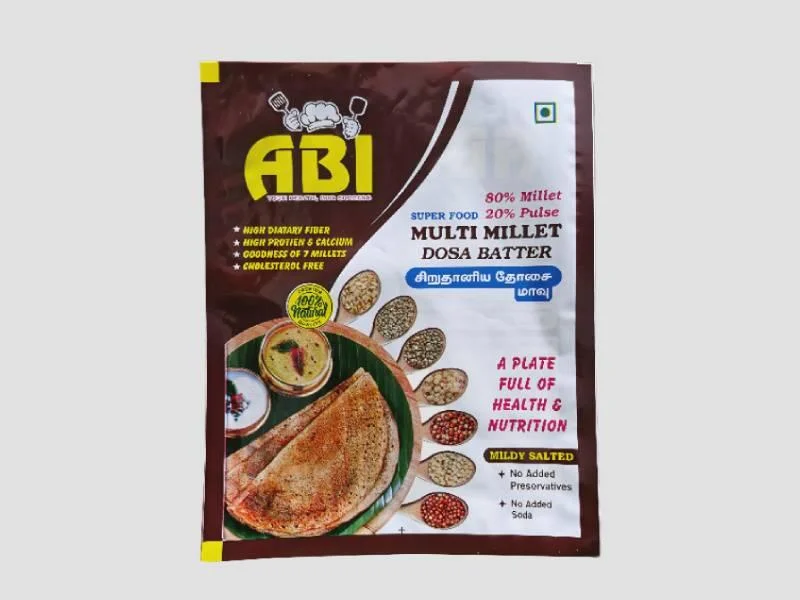
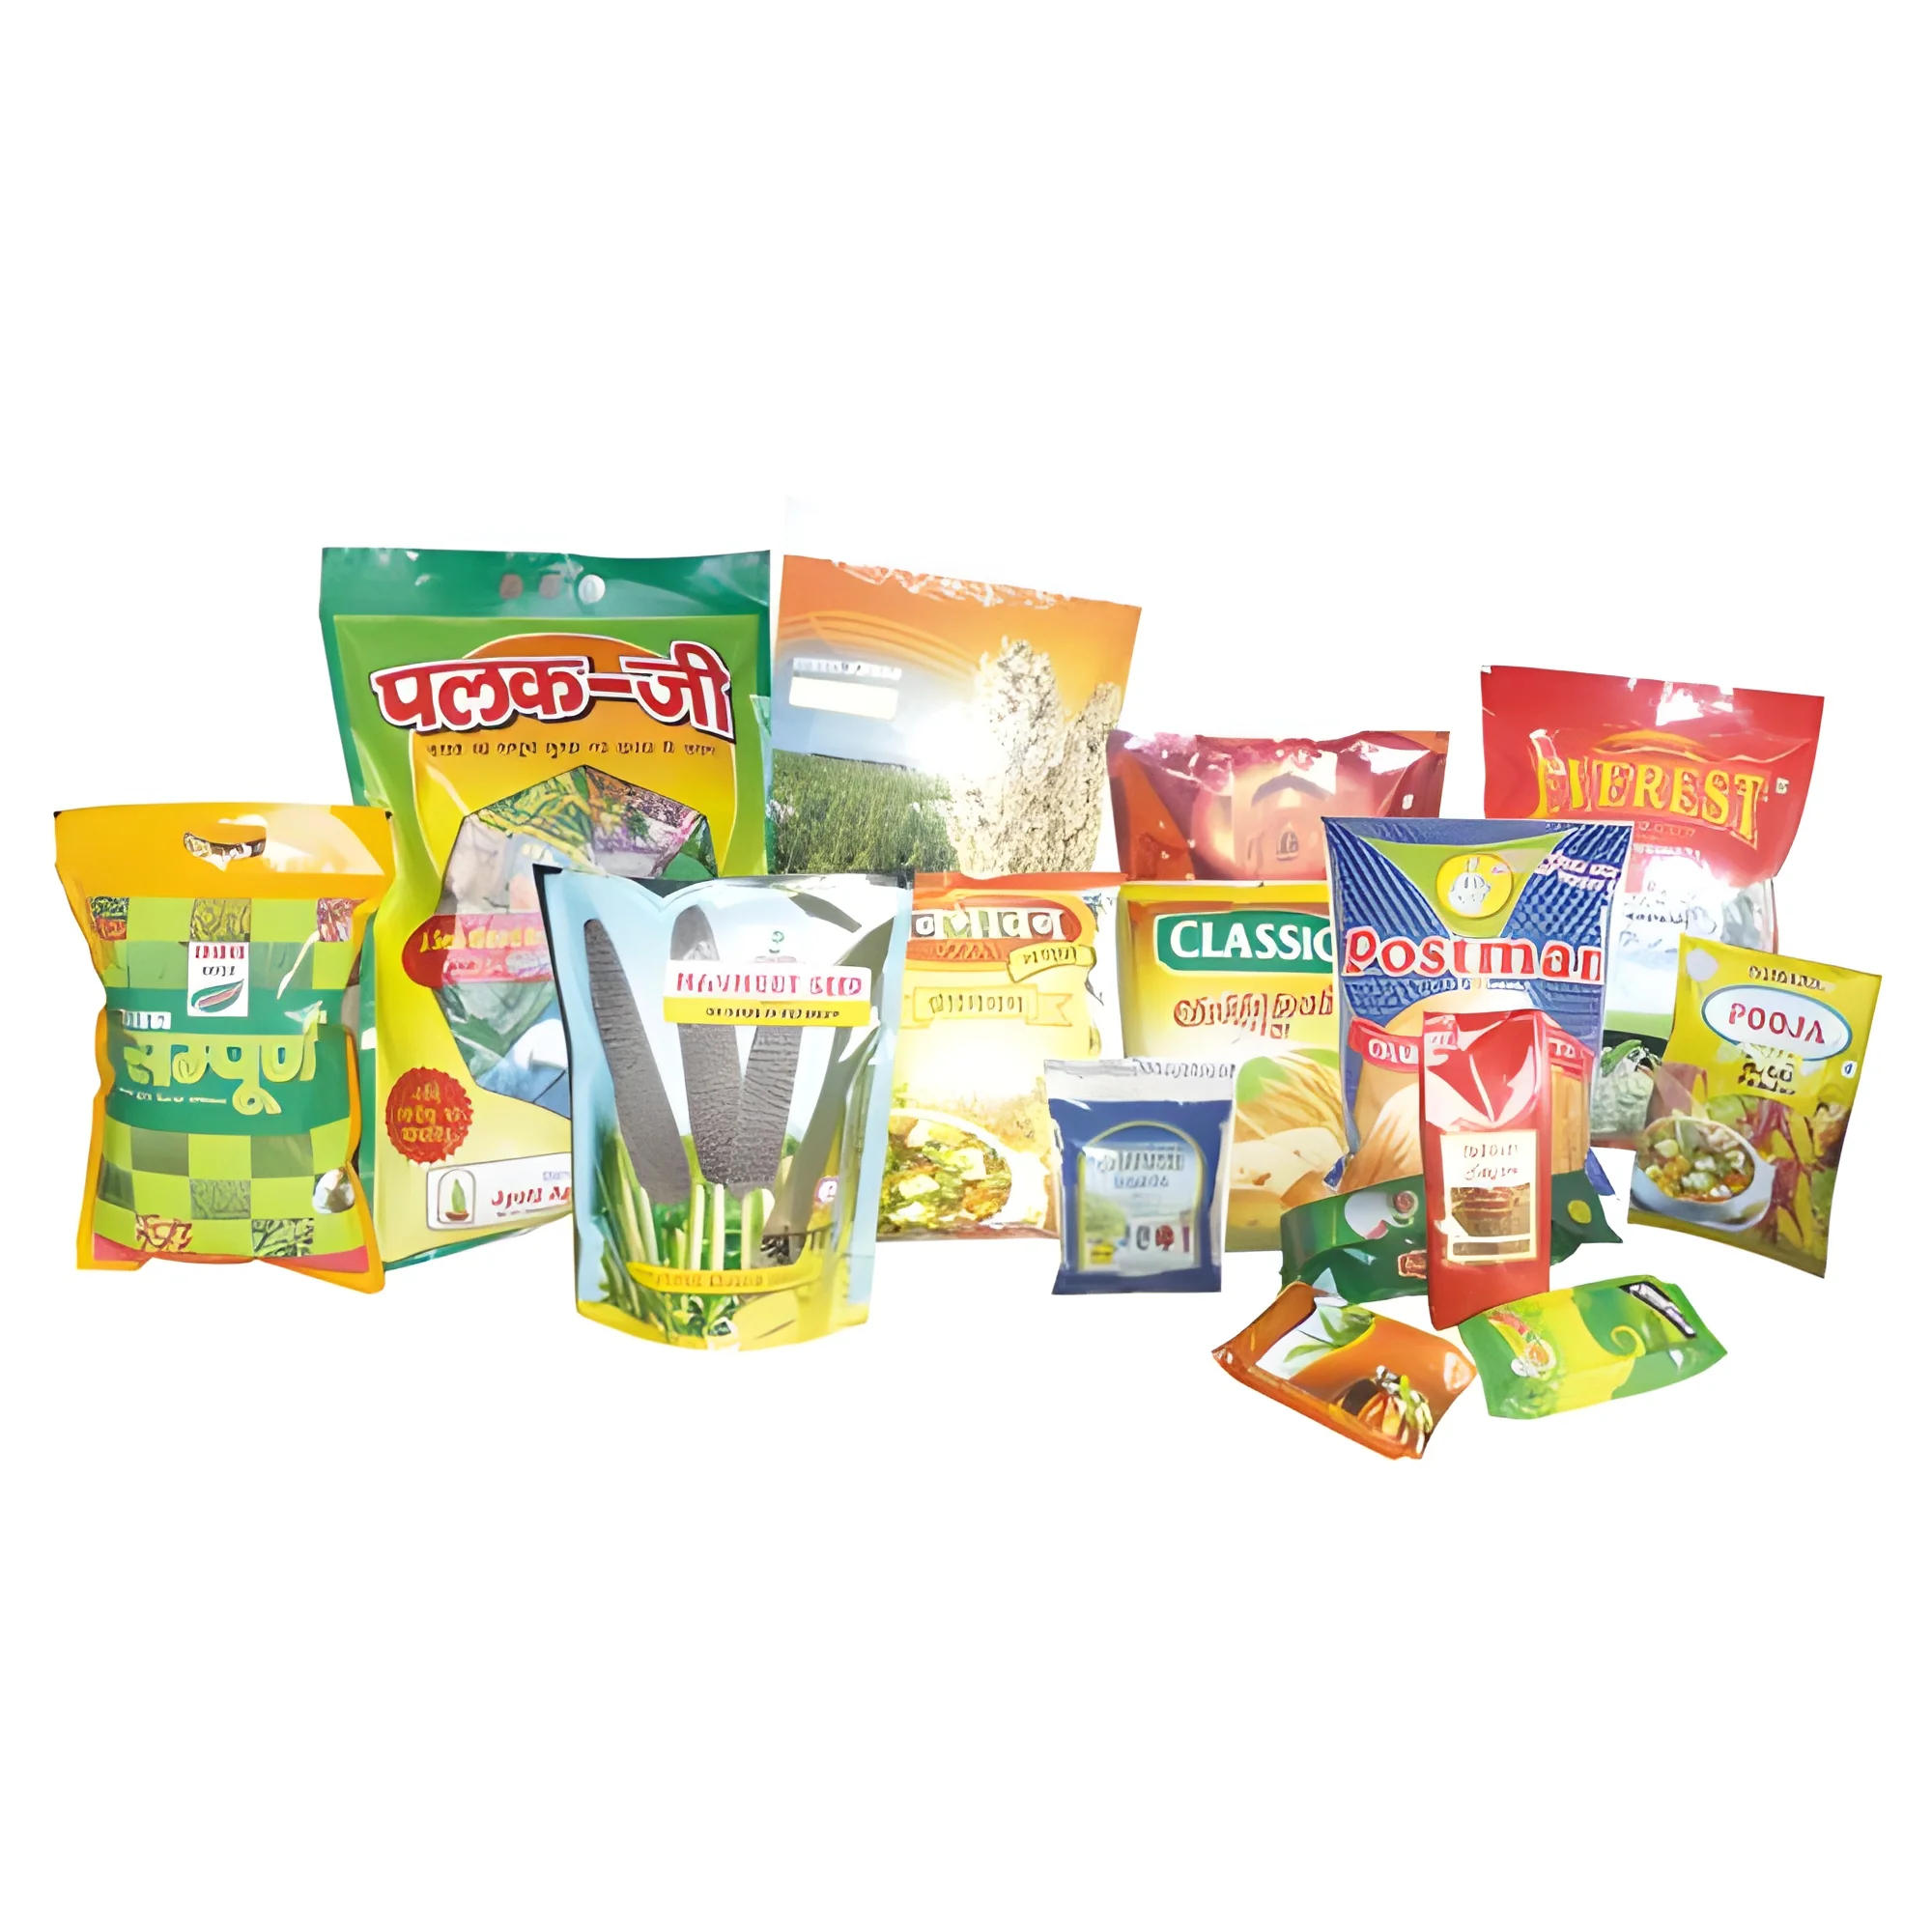
Pouches are flexible packaging solutions that are lightweight and versatile. They are commonly used for snacks, liquid products, and dry foods, providing excellent barrier properties.
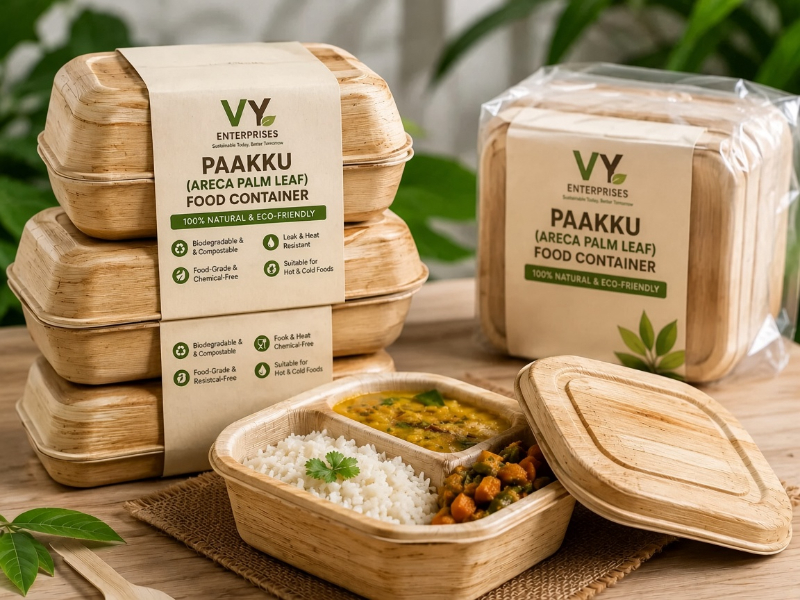
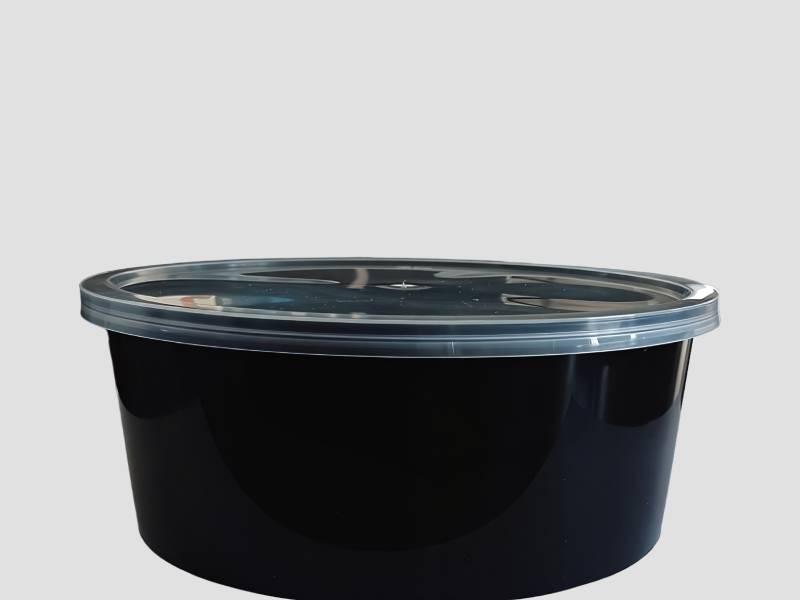
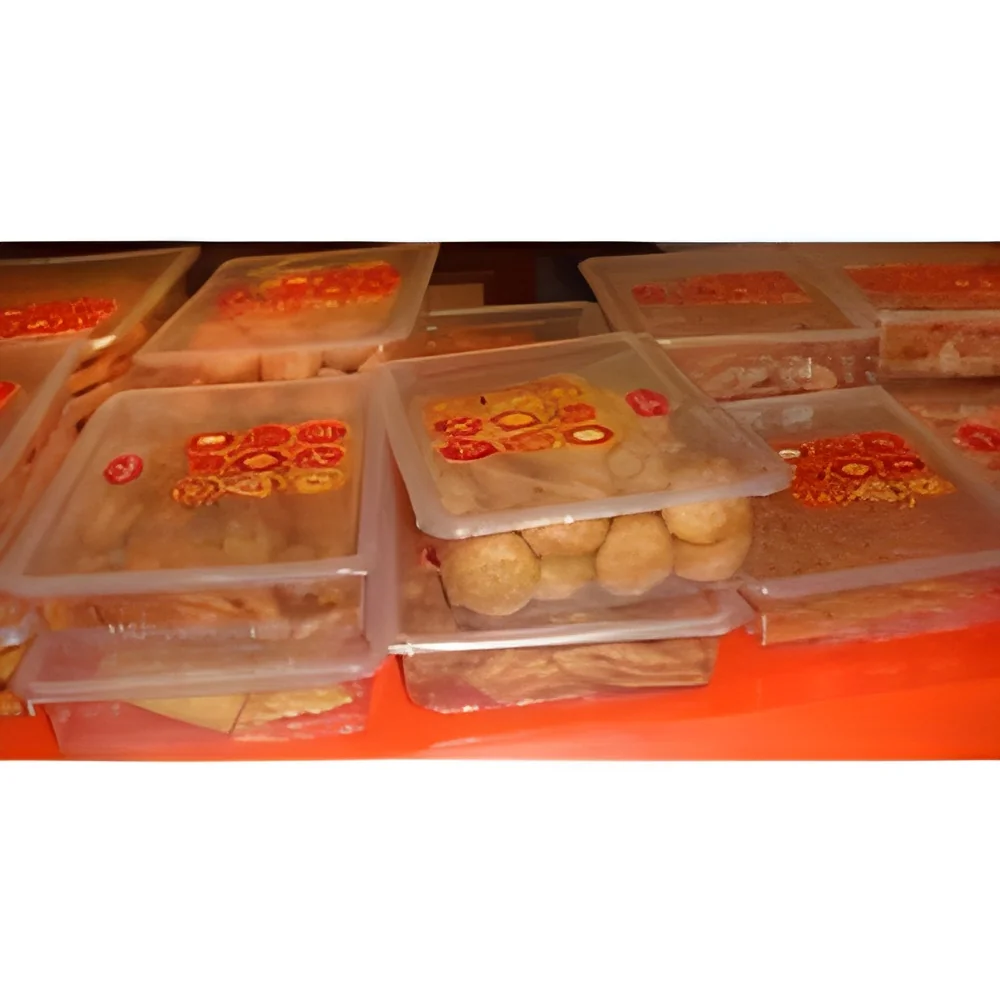
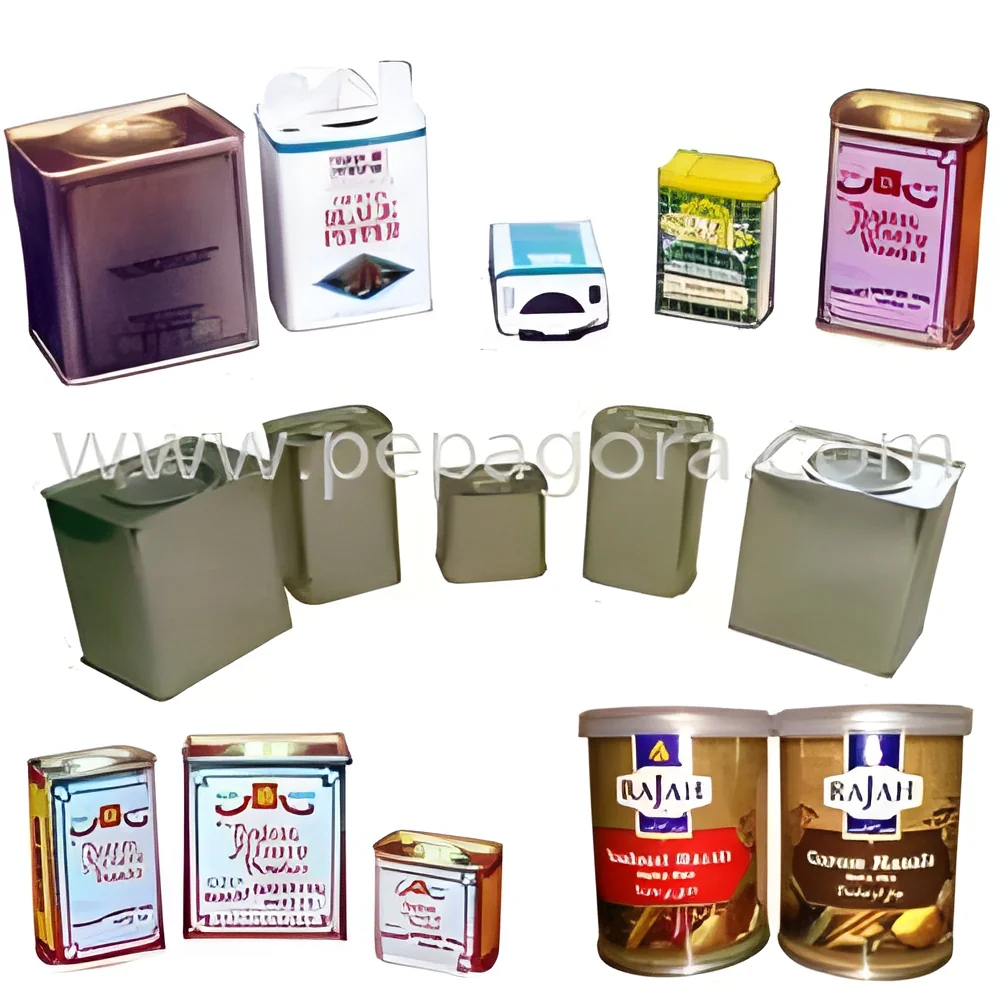
Containers
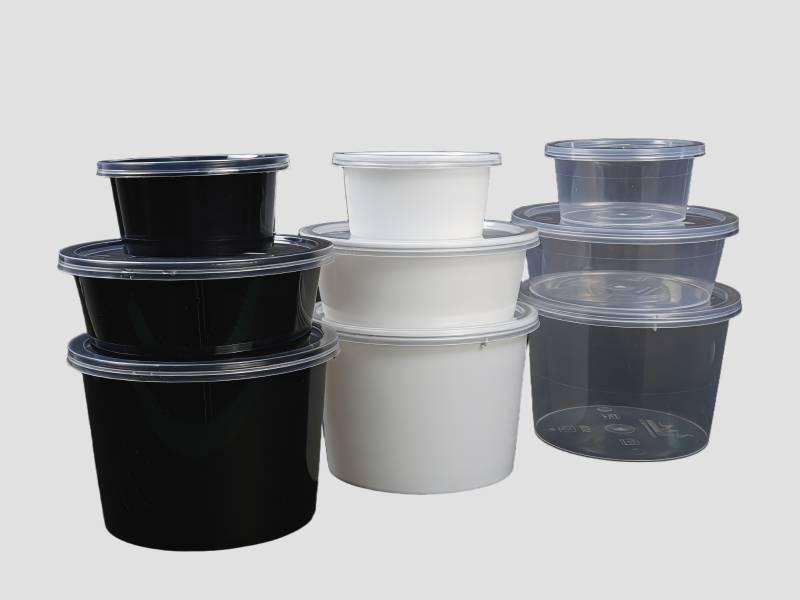
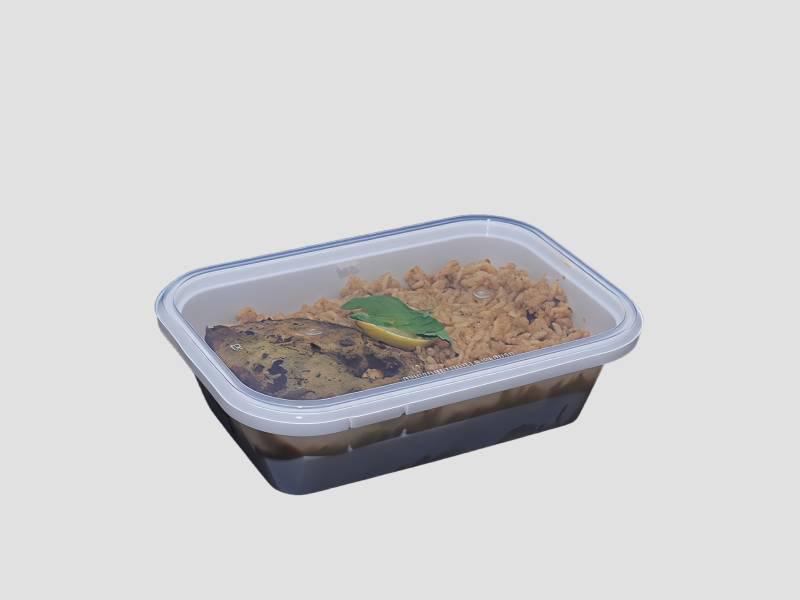
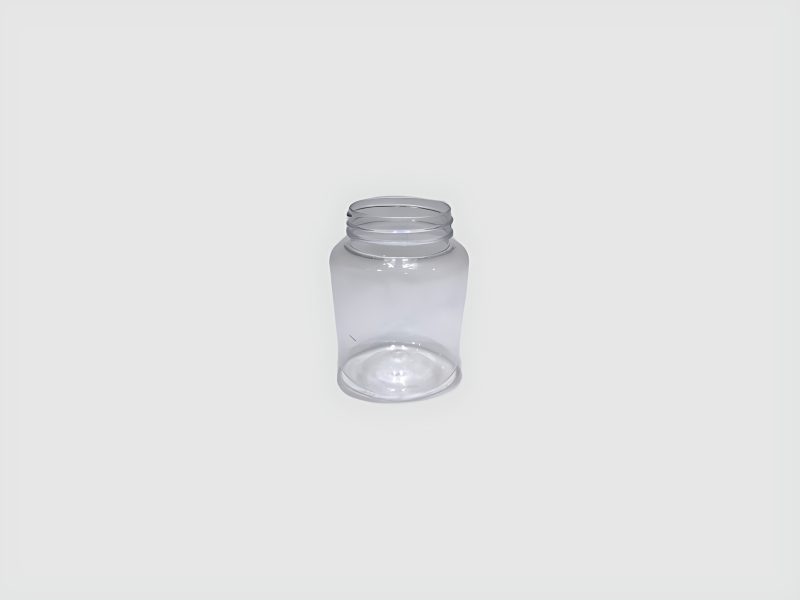
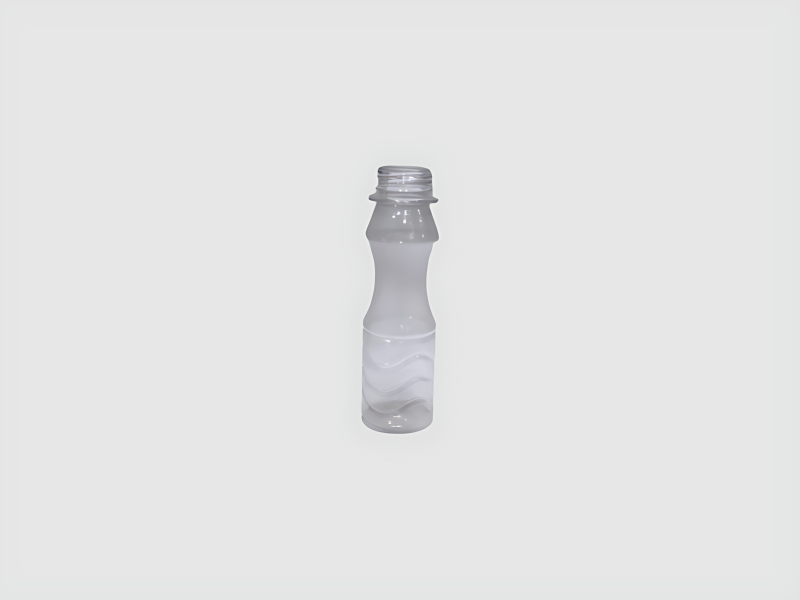
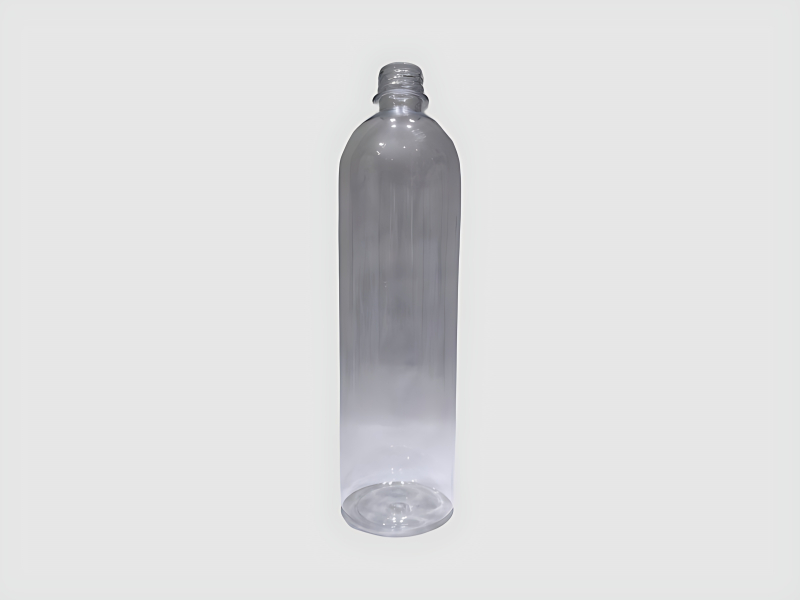
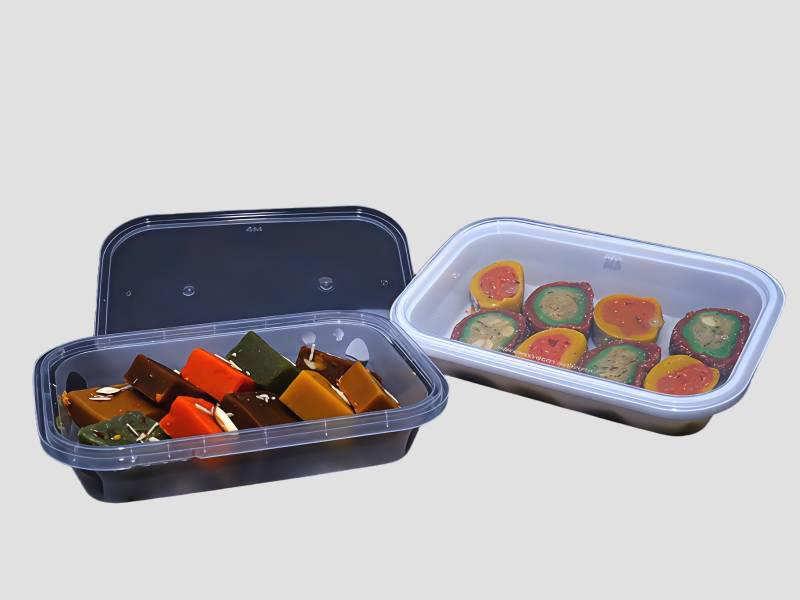
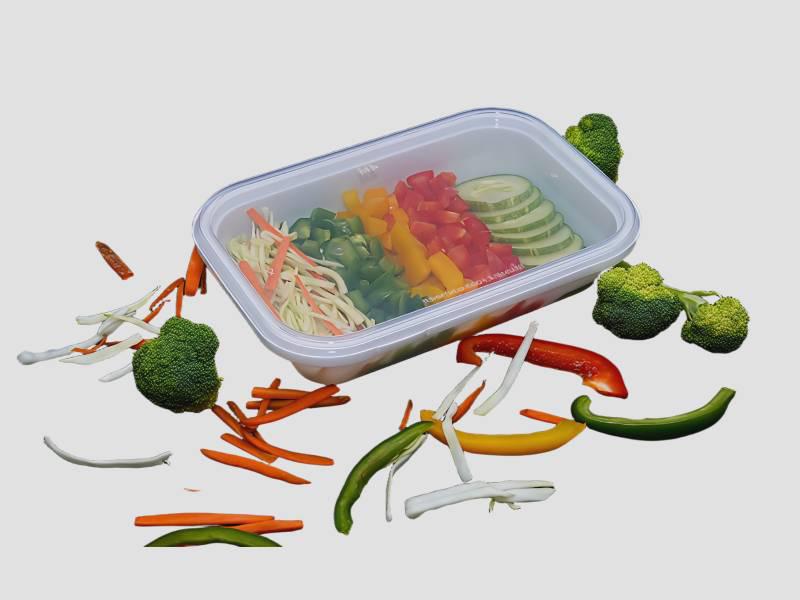
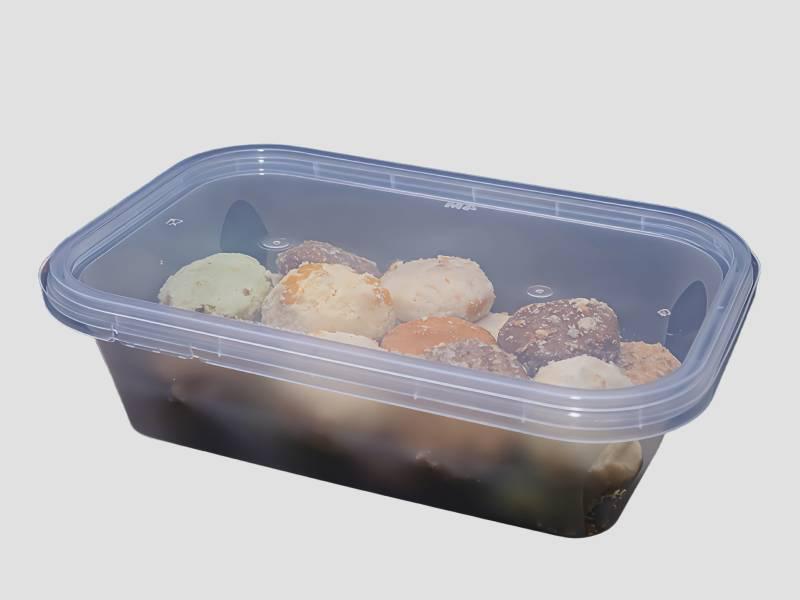
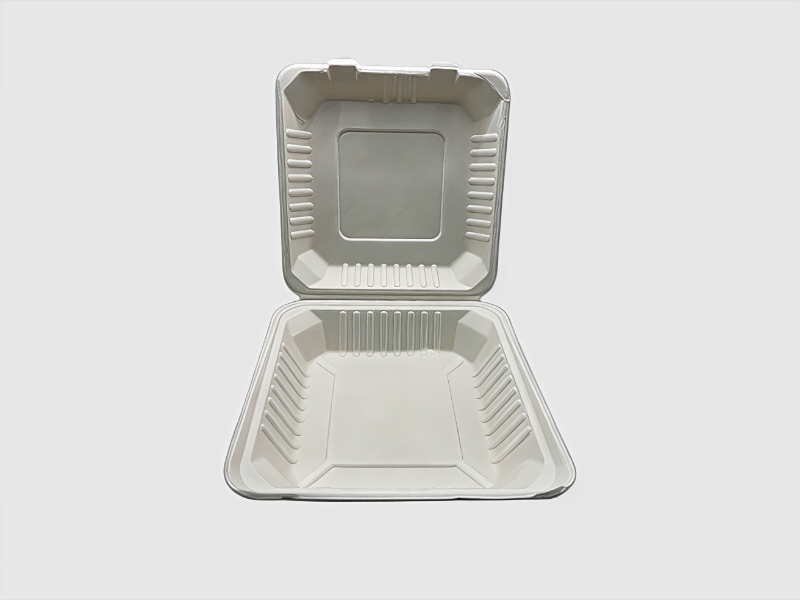
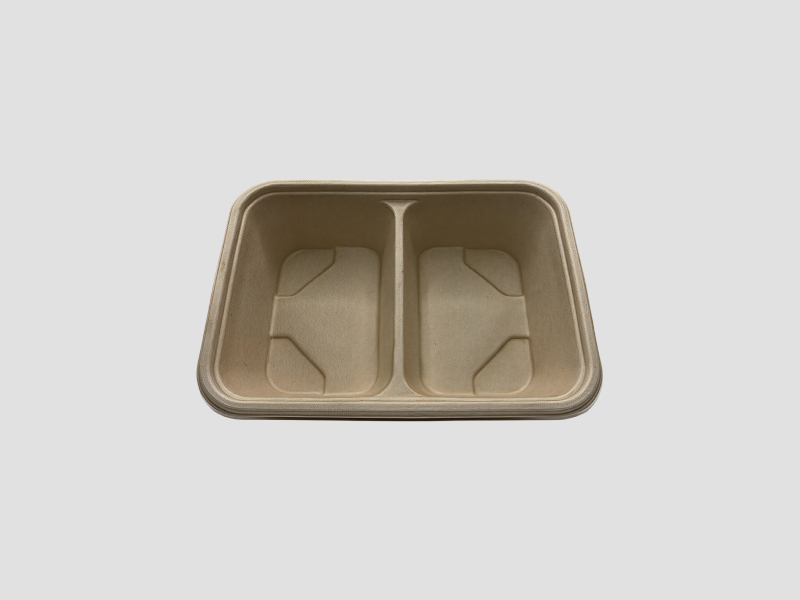
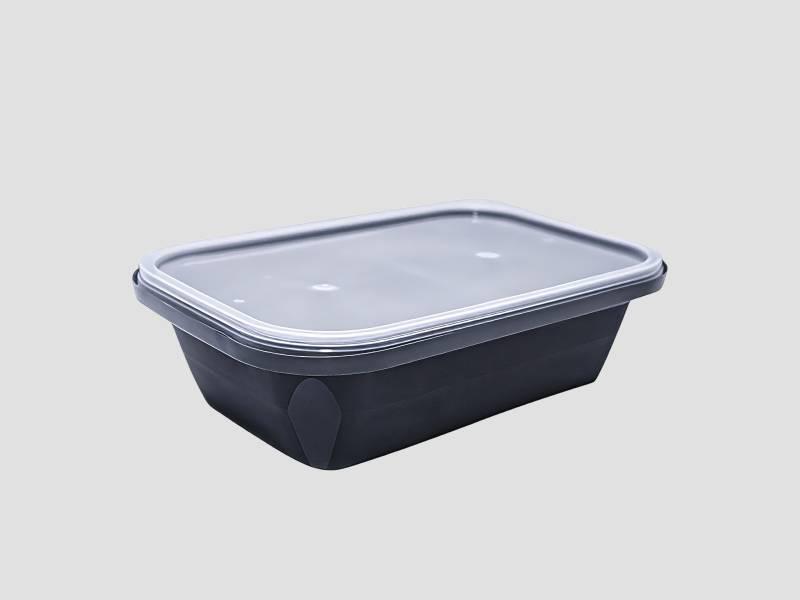
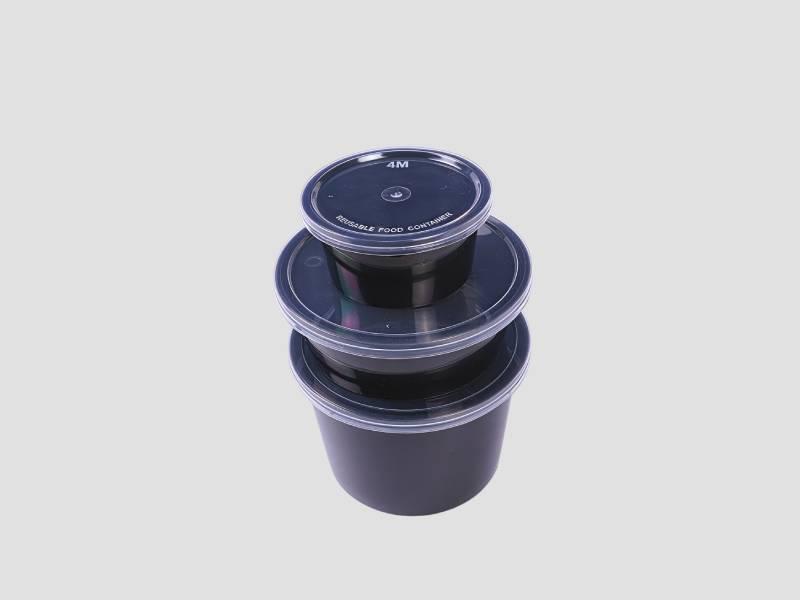
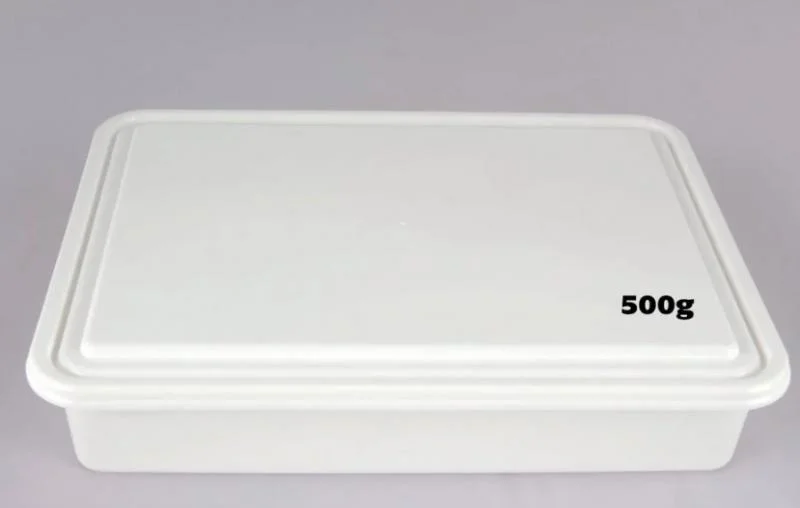
Containers are rigid packaging options ideal for bulk items, frozen foods, and meal kits. They offer strength and durability, ensuring safe storage and distribution.
Films
Films are thin, flexible materials used for wrapping and sealing food products. They provide moisture and oxygen barriers while allowing for visibility.
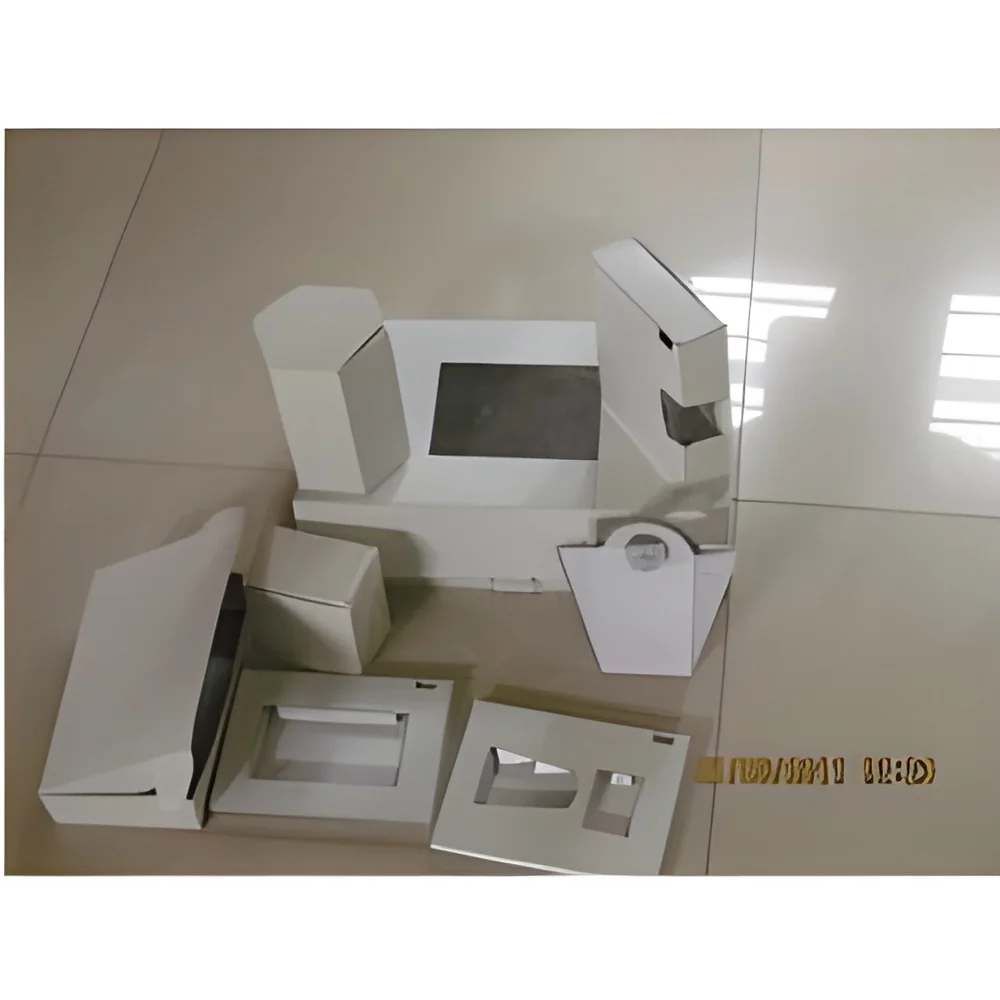
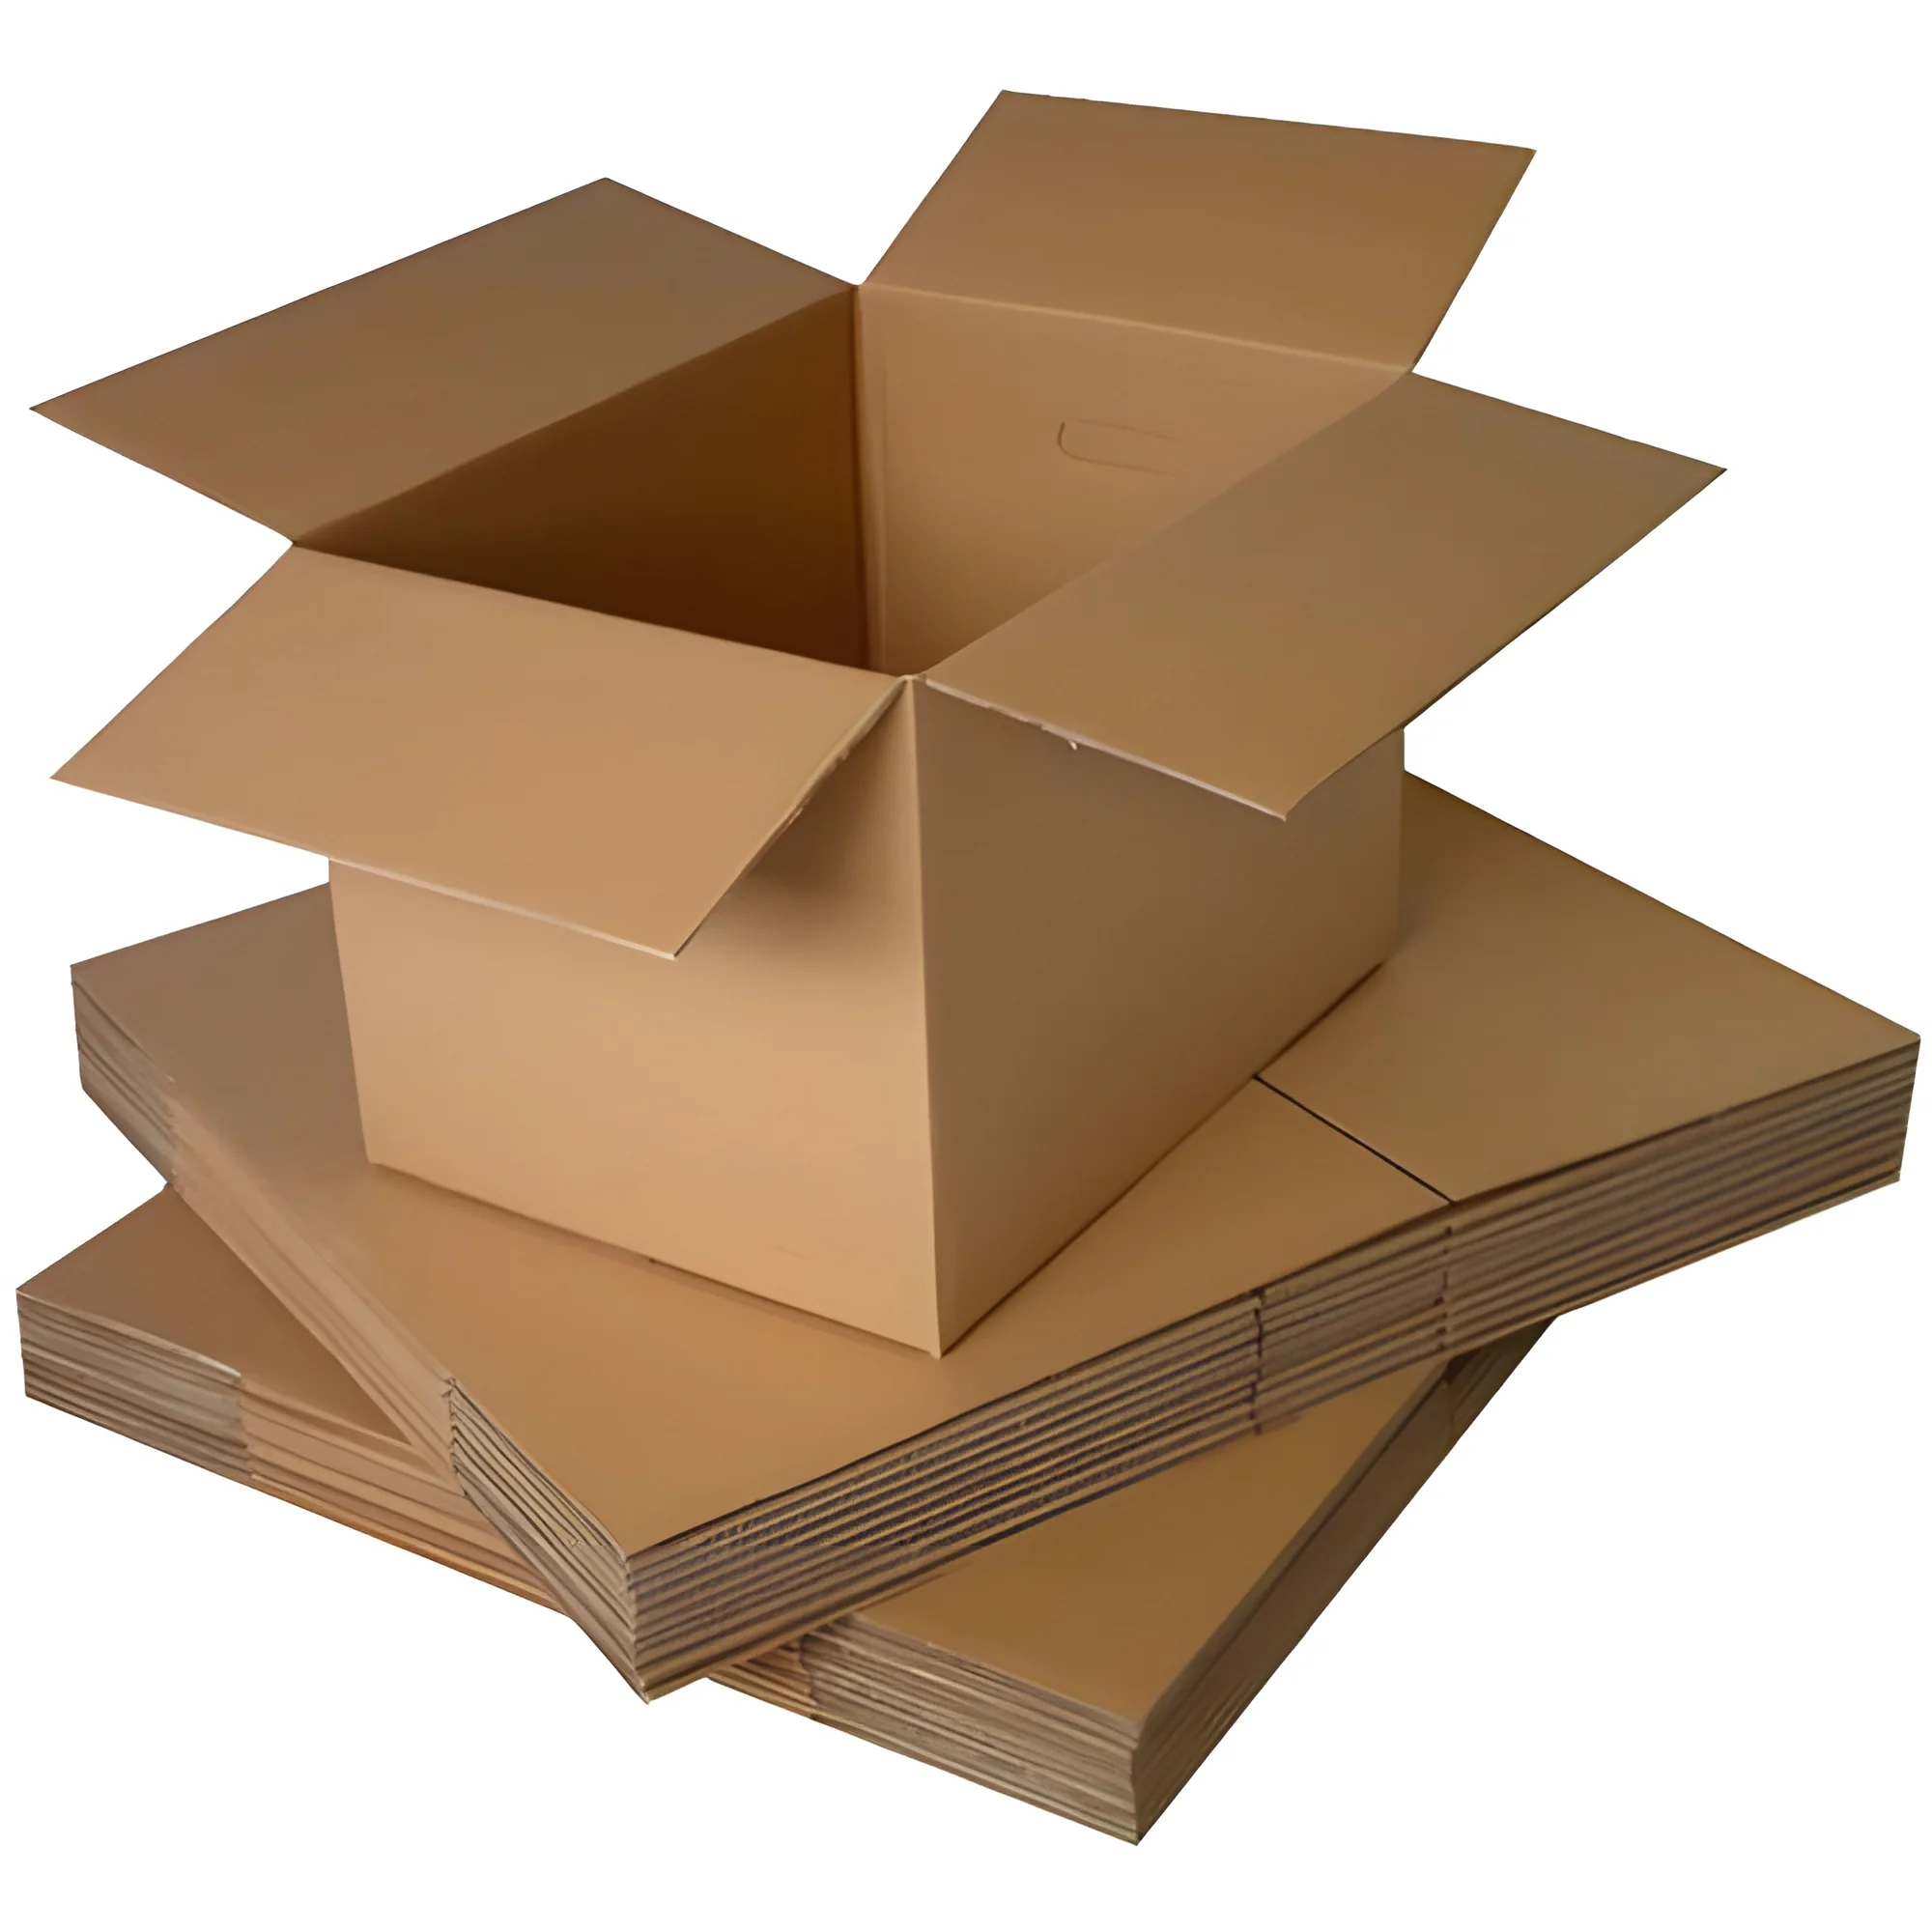
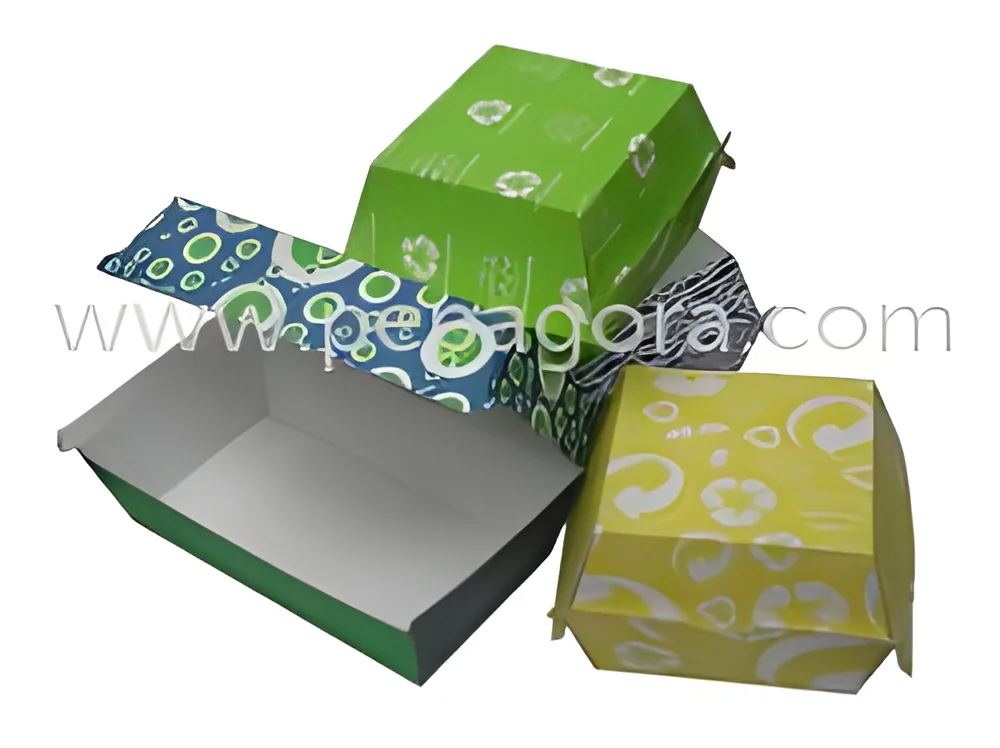
Boxes
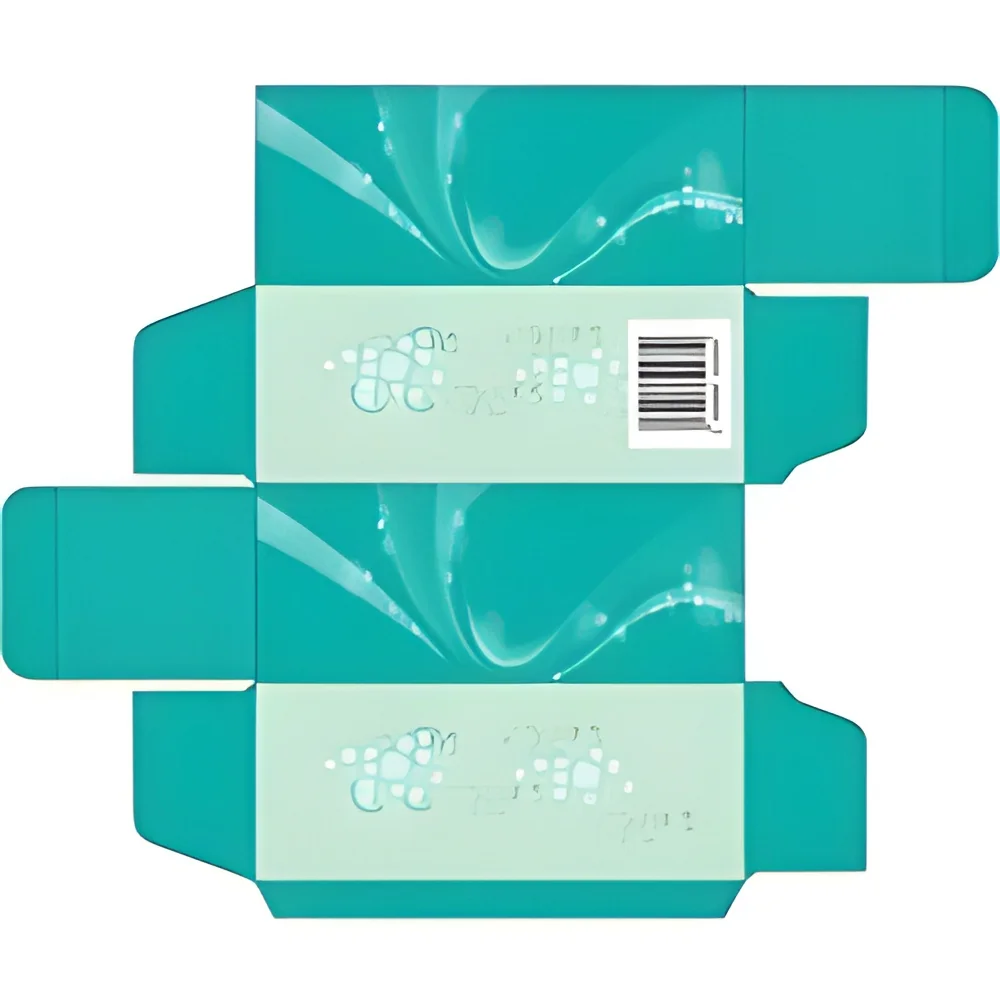
Boxes offer structural support for various food items, including baked goods and prepared meals. They are often used for retail packaging and can be customized with branding.
𝗕𝗲𝗻𝗲𝗳𝗶𝘁𝘀 𝗮𝗻𝗱 𝗔𝗱𝘃𝗮𝗻𝘁𝗮𝗴𝗲𝘀
Food Grade Packaging presents numerous advantages for businesses in the food sector.
Key benefits include:
1. Safety Assurance: Ensures food products are safe for consumption by preventing contamination.
2. Extended Shelf Life: Helps maintain freshness and quality, reducing food waste.
3. Compliance with Regulations: Adheres to local and international food safety standards, minimizing legal risks.
4. Branding Opportunities: Customizable options allow businesses to enhance brand visibility and appeal.
5. Cost Efficiency: Reduces spoilage and waste, leading to lower overall costs.
6. Environmental Considerations: Many options are eco-friendly, aligning with sustainable business practices.
𝗕𝘂𝘆𝗶𝗻𝗴 𝗚𝘂𝗶𝗱𝗲 𝗳𝗼𝗿 𝗕𝟮𝗕 𝗕𝘂𝘆𝗲𝗿𝘀
When sourcing Food Grade Packaging, businesses should carefully consider various factors to ensure they make informed purchasing decisions.
1. Quality Assessment: Evaluate the materials used in Food Grade Packaging to ensure they meet safety standards and are suitable for your products.
2. Supplier Verification: Conduct due diligence on suppliers to ensure they have a proven track record of reliability and compliance with industry standards.
3. Pricing and MOQ: Analyze pricing structures and minimum order quantities to align with budgetary constraints and operational needs.
4. Delivery and Lead Times: Consider logistics and the supplier's ability to meet your delivery requirements to avoid disruptions in your supply chain.
5. Compliance Requirements: Ensure the packaging meets all necessary regulatory requirements specific to your location and the types of food products being packaged.
𝗖𝗼𝗺𝗽𝗹𝗶𝗮𝗻𝗰𝗲 𝗮𝗻𝗱 𝗖𝗲𝗿𝘁𝗶𝗳𝗶𝗰𝗮𝘁𝗶𝗼𝗻𝘀
Compliance and certifications are crucial in the Food Grade Packaging industry to ensure safety and quality.
Relevant quality standards such as ISO 9001 guarantee that manufacturers adhere to consistent quality management practices. Additionally, the Hazard Analysis Critical Control Point (HACCP) framework is often implemented to identify and mitigate risks associated with food safety throughout the production process.
Industry certifications, like CE marking, indicate that products meet European safety standards. This is particularly important for businesses operating in or exporting to regions with stringent regulations.
Safety and testing requirements also play a significant role in compliance. Packaging must undergo various tests to ensure it does not leach harmful substances into food or compromise food safety.
Regional compliance considerations may also vary, requiring businesses to be aware of local regulations that govern food packaging materials and safety.
𝗪𝗵𝘆 𝗦𝗼𝘂𝗿𝗰𝗲 𝗙𝗼𝗼𝗱 𝗚𝗿𝗮𝗱𝗲 𝗣𝗮𝗰𝗸𝗮𝗴𝗶𝗻𝗴 𝗳𝗿𝗼𝗺 𝗣𝗲𝗽𝗮𝗴𝗼𝗿𝗮?
Pepagora provides a trusted platform for sourcing Food Grade Packaging with several key advantages.
Verified Supplier Network: Pepagora boasts a network of verified suppliers, ensuring that businesses can access high-quality packaging solutions from reputable manufacturers. This network helps buyers find reliable partners in the food packaging industry.
Streamlined RFQ Process: The Request for Quotation (RFQ) process is designed to be straightforward and efficient. This allows buyers to quickly obtain multiple quotes from suppliers, facilitating informed decision-making.
Trade Assurance and Support: Pepagora offers trade assurance to protect buyers throughout the sourcing process. This support helps to mitigate risks and provides peace of mind when making significant purchasing decisions.
Regional Coverage: With a strong presence in India, the GCC, and Southeast Asia, Pepagora connects buyers with suppliers across diverse geographic regions. This regional coverage ensures that businesses can find suitable Food Grade Packaging solutions tailored to their market needs.
By choosing Pepagora, businesses can confidently source Food Grade Packaging that meets their specific requirements while benefiting from a reliable and efficient procurement process.



Frequently Asked Questions
What are Food Grade Packaging?
Food Grade Packaging refers to materials used to package food products that meet specific safety and health regulations. These materials are designed to prevent contamination and preserve the quality and freshness of food items.
What are the different types of Food Grade Packaging?
The different types of Food Grade Packaging include flexible packaging, rigid containers, vacuum-sealed packs, and aseptic packaging. Each type serves unique purposes based on the food product's requirements, such as shelf-life, durability, and protection.
How do I choose the right Food Grade Packaging?
Choosing the right Food Grade Packaging involves considering factors like the type of food, storage conditions, and shelf-life requirements. It is also important to assess the material's compatibility with the food product to ensure safety and quality.
What are the standard specifications for Food Grade Packaging?
Standard specifications for Food Grade Packaging include compliance with FDA or FSSAI regulations, material safety, and performance criteria such as barrier properties and durability. Packaging must also be tested for migration limits to ensure no harmful substances leach into the food.
What is the price range for Food Grade Packaging?
The price range for Food Grade Packaging can vary significantly based on material, design, and order volume. Typically, prices can range from a few rupees for simple packaging types to several hundred rupees for specialized solutions.
What quality standards apply to Food Grade Packaging?
Quality standards for Food Grade Packaging include compliance with ISO 22000 and other food safety management systems. Additionally, packaging must meet specific health and safety regulations set by authorities like the FDA and FSSAI to ensure it is safe for food contact.
Where can I find Food Grade Packaging suppliers in India?
You can find Food Grade Packaging suppliers in India through B2B marketplaces like Pepagora, industry trade shows, and online directories. It's advisable to check supplier credentials and product certifications to ensure quality.
Can Food Grade Packaging be customized?
Yes, Food Grade Packaging can be customized to meet specific requirements such as size, design, and branding. Customization options may vary by supplier, so it's important to communicate your needs clearly.
What is the typical minimum order quantity for Food Grade Packaging?
The typical minimum order quantity (MOQ) for Food Grade Packaging can vary widely based on the supplier and product type. Generally, MOQs can range from a few hundred to several thousand units.
What is the typical lead time for Food Grade Packaging?
The typical lead time for Food Grade Packaging usually ranges from 2 to 6 weeks, depending on the type of packaging, customization requirements, and supplier capacity. It is advisable to confirm lead times with your supplier when placing an order.
Why Businesses Trust Pepagora
Thousands of companies trust Pepagora to source smarter and sell faster
Expand Your Sales Globally
Source Smarter,Grow Faster